Raw Material Control & Paddy Procurement
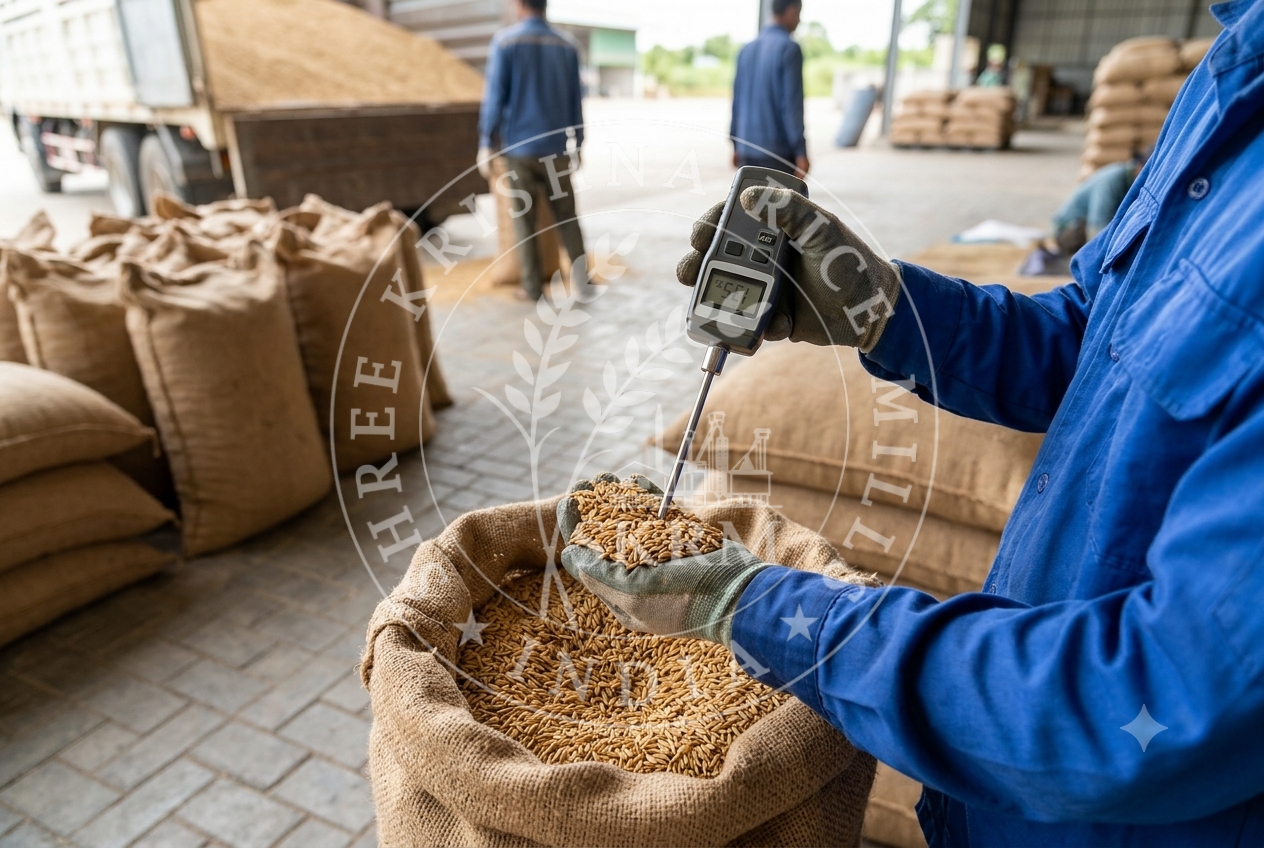
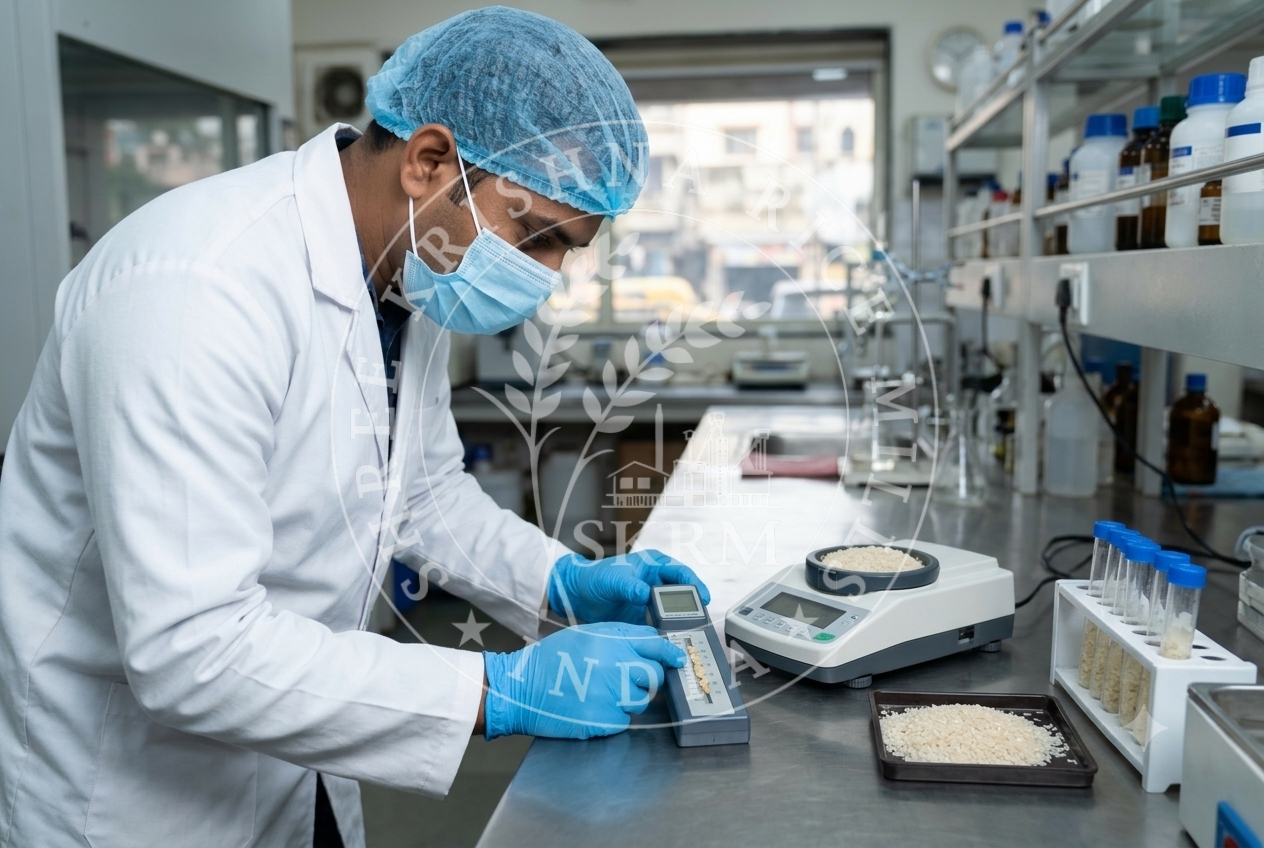
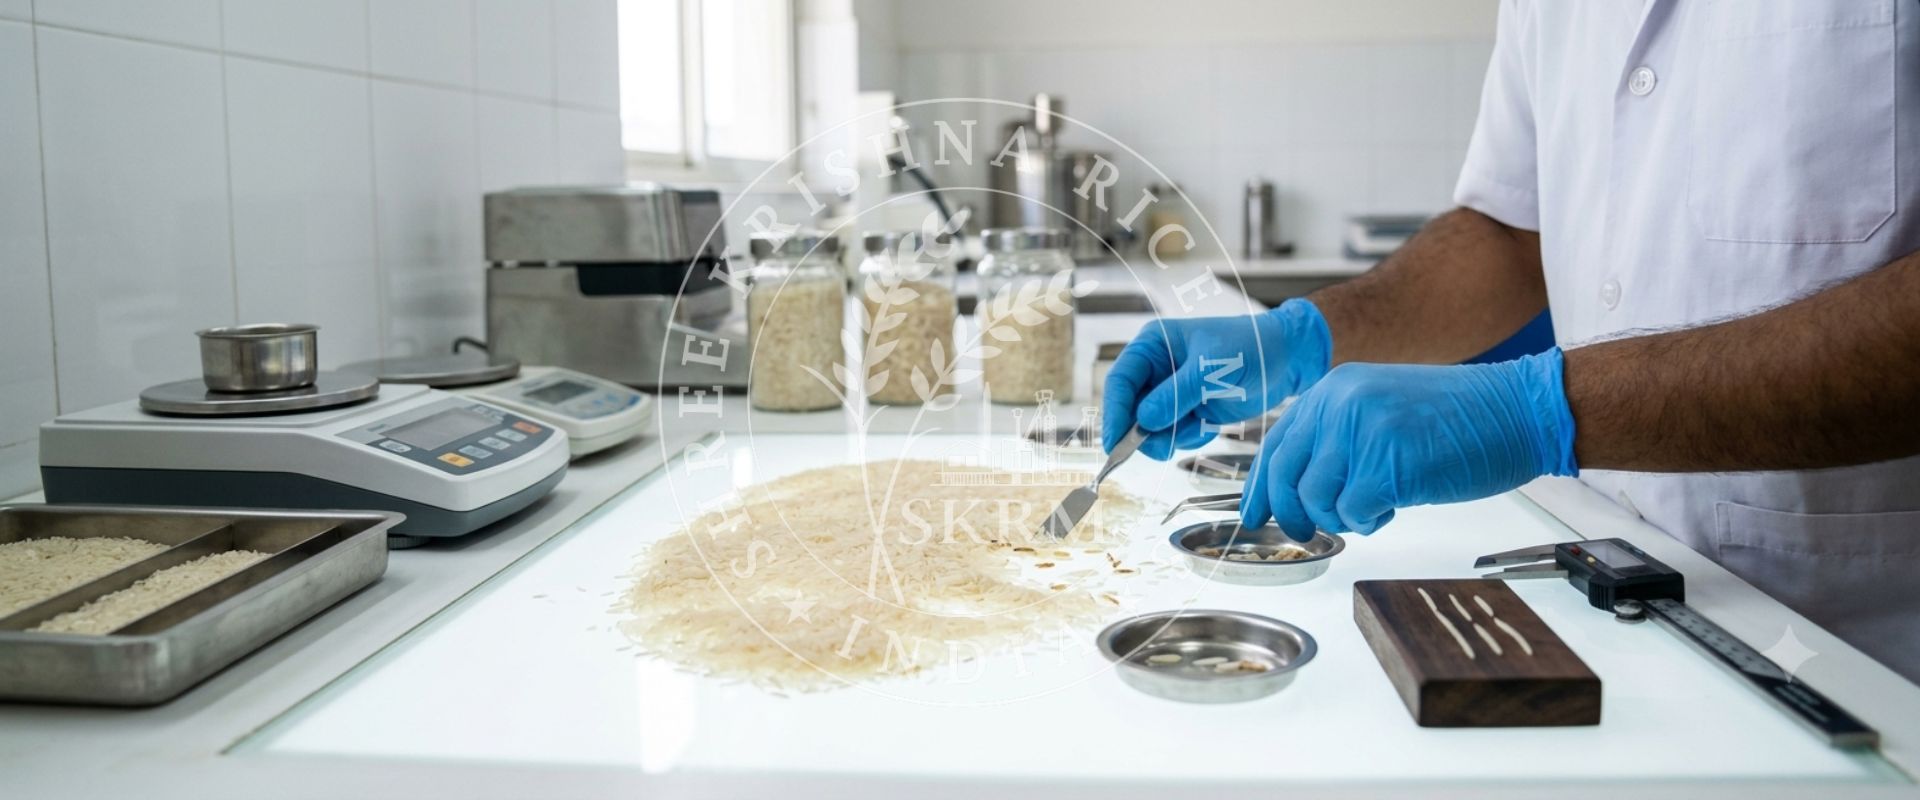
Quality begins at the farm gate. Our certified agricultural inspectors test incoming paddy directly from verified mandis across Northern India. Samples undergo rigorous physical verification before unloading.

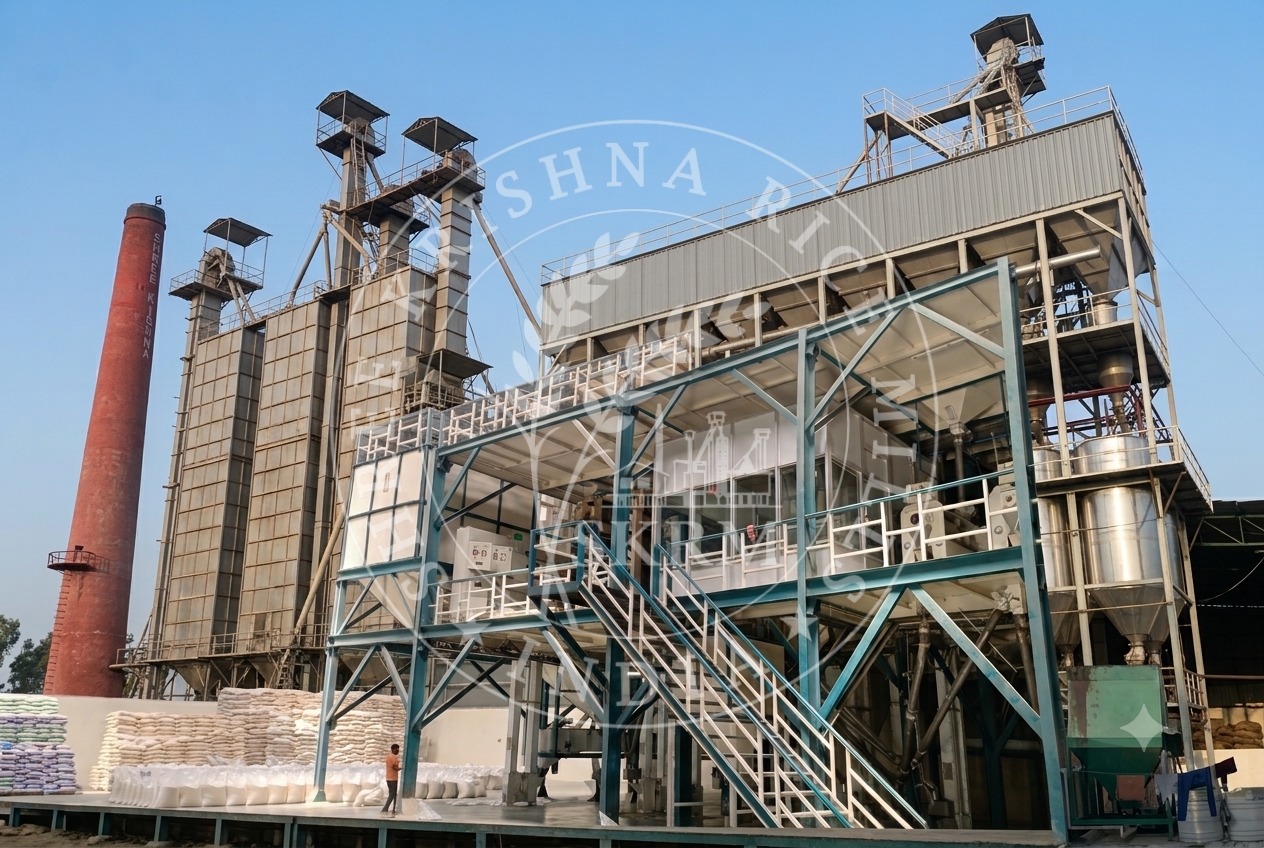
At Shree Krishna Rice Mills (SKRM India), quality control is integrated into every stage of our rice manufacturing process. From raw paddy selection and moisture-controlled aging to high-precision Sortex optical grading and final export dispatch, we ensure strict physical, chemical, and destination-specific compliance for global buyers.
An end-to-end 10-step precision pipeline ensuring zero non-conformity from farm procurement to container sealed dispatch.
Comprehensive breakdown of our technical parameters and testing regimes.
Quality begins at the farm gate. Our certified agricultural inspectors test incoming paddy directly from verified mandis across Northern India. Samples undergo rigorous physical verification before unloading.


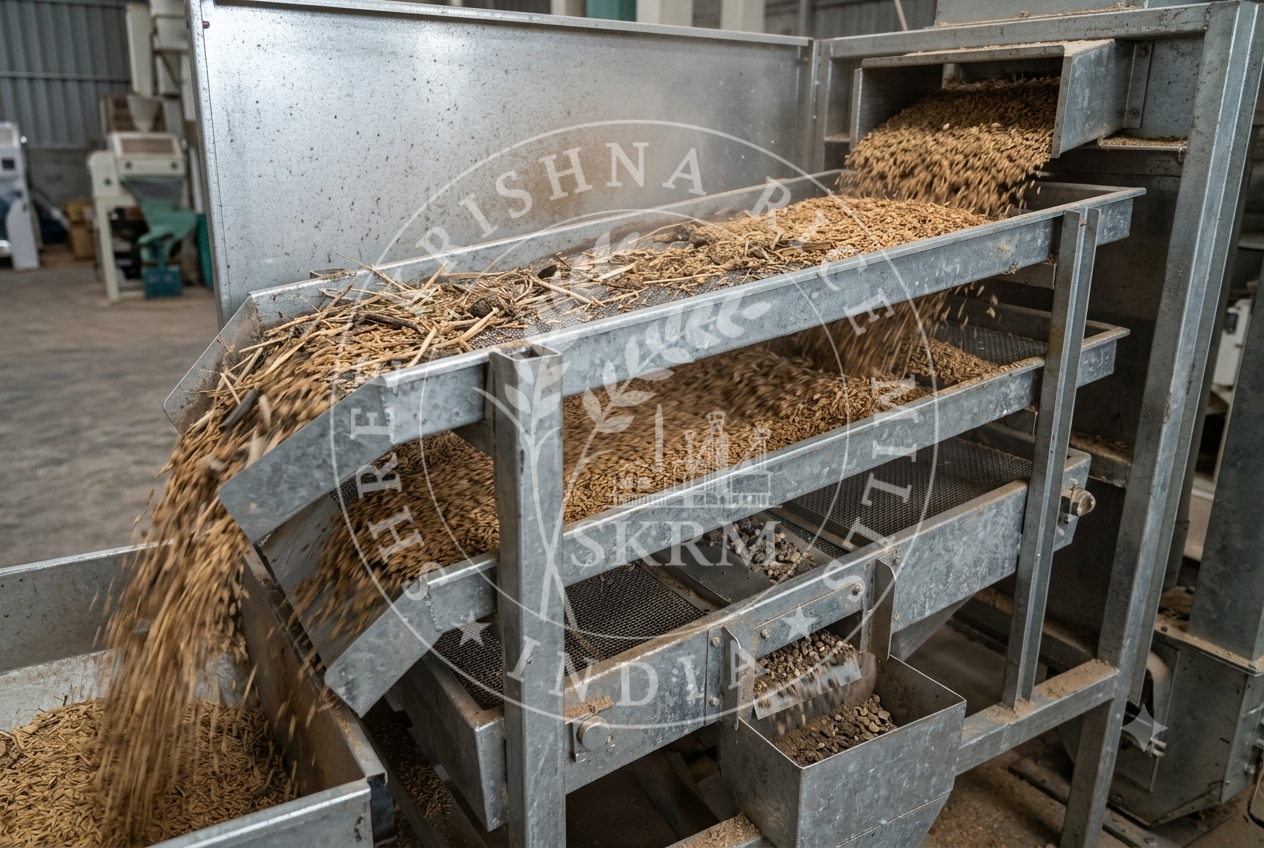
Automated multi-stage cleaning removes all light impurities, dust, stones, and iron particles using heavy-duty aspirators, destoners, and magnetic separators to safeguard downstream milling equipment and ensure pristine cleanliness.
We operate specialized processing lines designed to alter starch structures according to exact commercial requirements, enhancing cooking properties, aroma retention, and kernel strength.

Rubber roll huskers and vertical friction polishers gently strip outer husk layers without cracking the starch matrix.
Multi-tier length graders and indented cylinder separators categorize grains by precise millimeter length parameters.
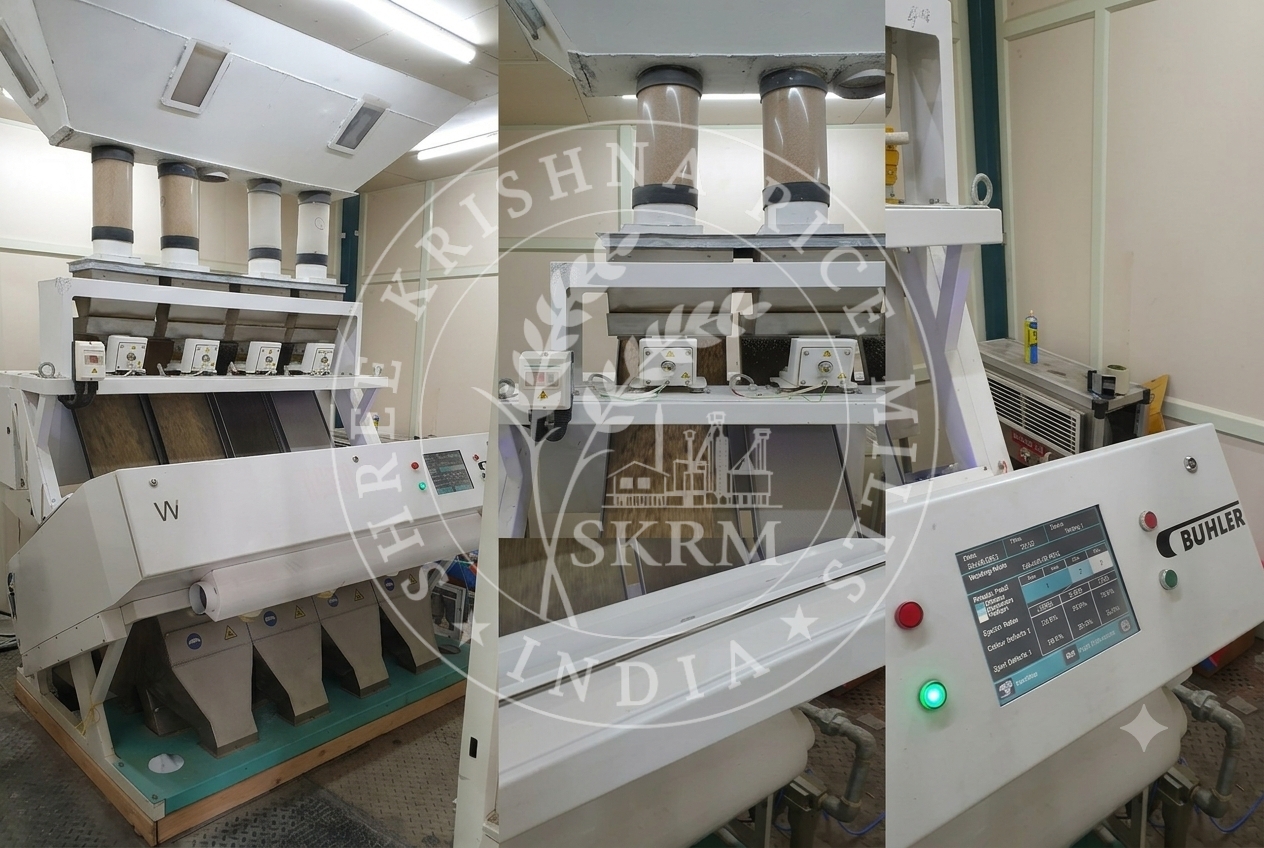
Equipped with full-spectrum trichromatic digital cameras and InGaAs NIR sensors, our optical sorters eject discolored grains, chalky kernels, yellow spots, peck grains, and minute glass or plastic fragments in milliseconds.

Moisture levels are continuously monitored with calibrated electric moisture meters. Keeping moisture content strictly below 12.5% prevents mold formation, insect infestation, and spoilage during ocean transportation.
Benchmarked against Agmark and Export Inspection Council (EIC) standards.
Every export batch is sampled and sent to NABL-accredited laboratory facilities (SGS, Intertek, Geo-Chem) to verify compliance with destination region Maximum Residue Limits (MRLs).

Automated check-weighers and barcode printers guarantee exact bag weights and flawless artwork execution.
Third-party surveyors (SGS, Bureau Veritas, Cotecna) conduct container seal inspections prior to port transit.
Customized physical specs, customized branding, and country-specific port clearances.
We match your target market price point with exact grain length, broken %, and processing type (Raw, Steam, Sella).
Full custom packaging customization: BOPP, Pouch, Non-Woven, Jute with multi-lingual label regulation compliance.
Dispatch of live production lot samples via DHL/FedEx for physical cooking and laboratory pre-approval.
Fumigated, SGS-inspected container loading with full phytosanitary and origin documentation dispatch.
Natural aged paddy, gentle milling to protect delicate natural aromatic oils. Strict chalkiness rejection.
Pass-through steam treatment hardens kernel outer shell, ensuring long fluffy non-sticky grains after cooking.
Deep water soaking locks nutrients into kernel core. High thermal endurance ideal for bulk catering.
Extended pressurized steaming imparts signature golden hue, firm texture, and supreme cooking yield.
Every consignment is dispatched with a comprehensive legal documentation packet for seamless import custom clearance: